Time: Oct 28 2026 Views: 16
Every day, industrial boilers, furnaces, kilns, and manufacturing processes release large amounts of thermal energy into the environment. Much of this energy leaves through hot exhaust gases, cooling water, and heated equipment surfaces.
Rather than allowing this energy to go unused, industrial facilities can capture and reuse part of it through waste heat recovery systems.
Waste heat recovery can reduce fuel consumption, improve energy efficiency, and lower operating costs. However, the appropriate technology depends on the temperature, composition, and availability of the waste heat source.
This article explains what waste heat recovery is, how waste heat recovery systems work, the role of waste heat recovery boilers, and how corrosion-resistant heat exchangers can support deeper heat recovery from industrial flue gas.
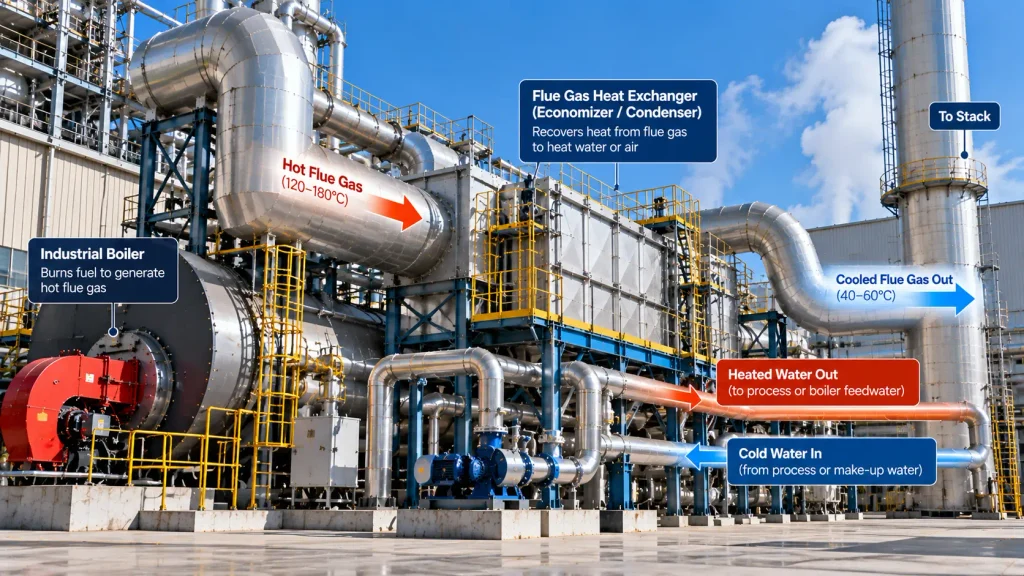
Waste heat recovery is the process of capturing thermal energy that would otherwise be discharged from an industrial process and reusing it for a useful purpose.
Waste heat can originate from many industrial operations, including combustion, chemical reactions, manufacturing, and power generation.
Common sources include:
Instead of releasing this energy directly into the environment, a waste heat recovery system transfers it to another process.
For example, hot boiler exhaust can be used to preheat boiler feedwater, while furnace exhaust can be used to warm incoming combustion air.
In both cases, recovered heat reduces the amount of additional energy required.
Industrial processes frequently operate at high temperatures, and a significant portion of the energy supplied may leave the process as unused heat.
According to the U.S. Department of Energy, industrial waste heat represents a substantial opportunity for improving energy productivity.
However, not all waste heat can be recovered economically. The practical recovery potential depends on the heat source, available temperature difference, operating hours, and demand for recovered energy.
The objective is therefore not simply to capture as much heat as possible, but to recover useful energy efficiently, safely, and reliably.
A waste heat recovery system captures energy from a hot industrial stream and transfers it to a cooler medium or energy conversion process.
The operating principle can be explained in five steps.
The process begins by identifying where useful thermal energy is being lost.
For industrial combustion equipment, this is often the exhaust gas leaving the boiler or furnace.
Engineers evaluate several parameters:
These conditions determine which recovery technologies are technically suitable.
A heat exchanger is installed between the waste heat source and the receiving medium.
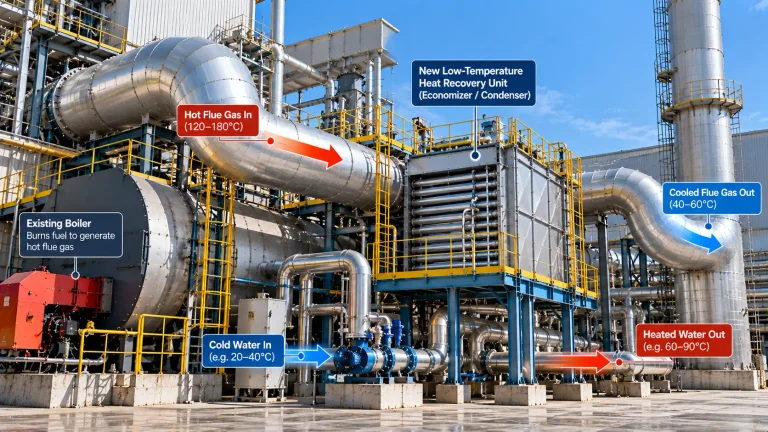
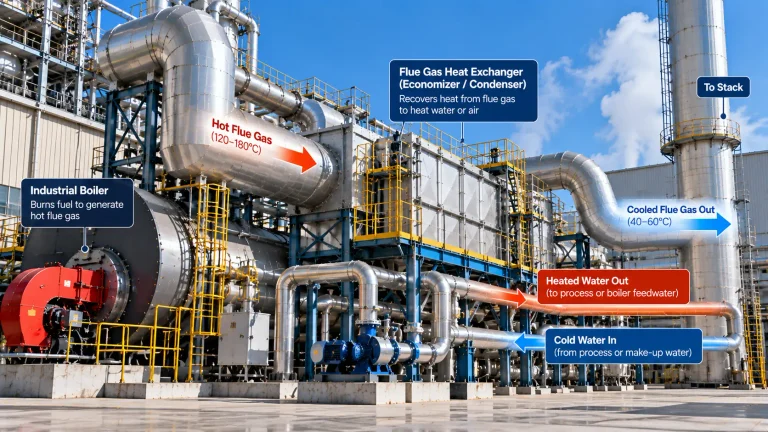
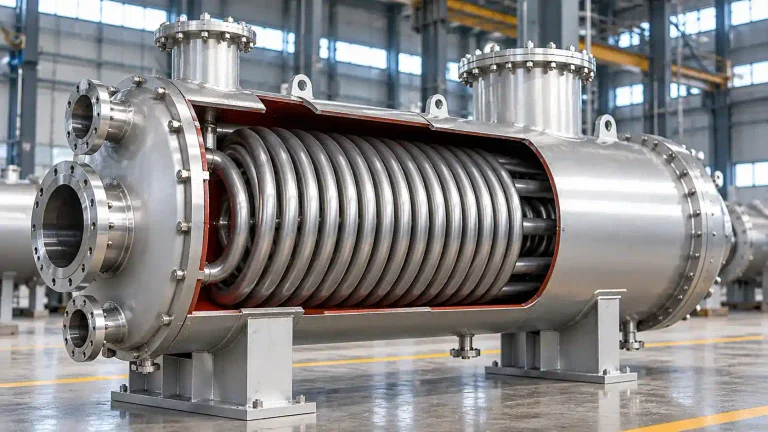
In a typical gas-to-water system, hot exhaust gas passes over heat transfer surfaces while cooler water flows through a separate circuit.
Heat transfers through the tube walls without the two fluids mixing.
As the exhaust gas cools, the water temperature increases.
The recovered energy may be used for:
The most suitable application depends on the temperature and quantity of recovered heat.
For example, low-temperature waste heat may be useful for preheating water, even when its temperature is insufficient for efficient steam generation.
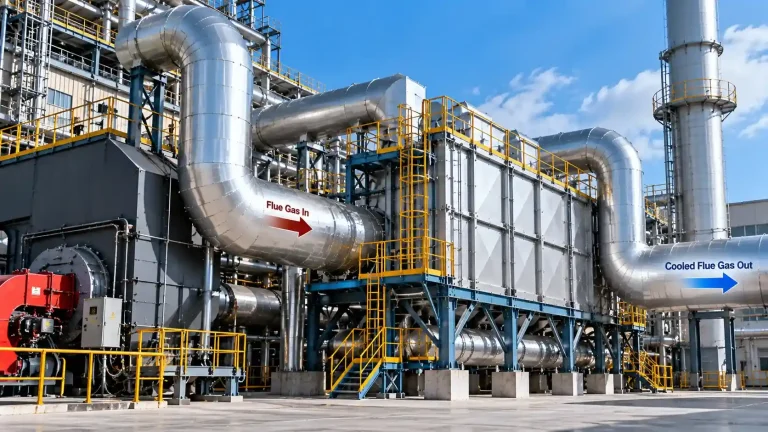
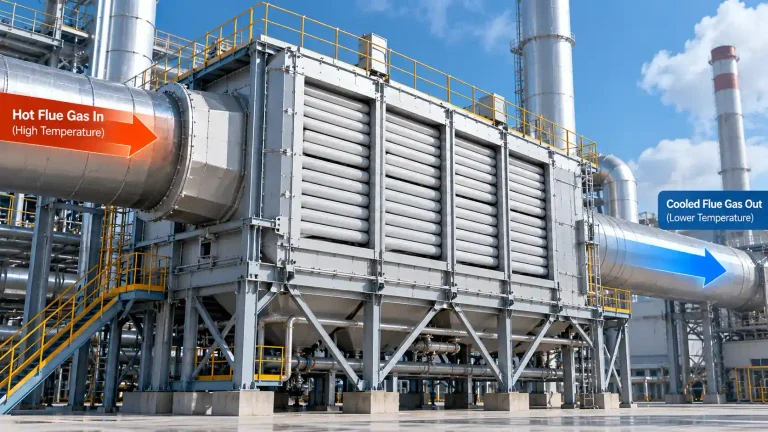
After heat transfer, the exhaust gas leaves the recovery equipment at a lower temperature.
The gas then continues to downstream treatment equipment or the exhaust stack.
System design must ensure that the recovery equipment does not create excessive pressure drop or interfere with the primary industrial process.
Industrial waste heat recovery systems require appropriate operating controls.
Temperature sensors, flow measurement, pressure monitoring, and control valves help maintain stable performance.
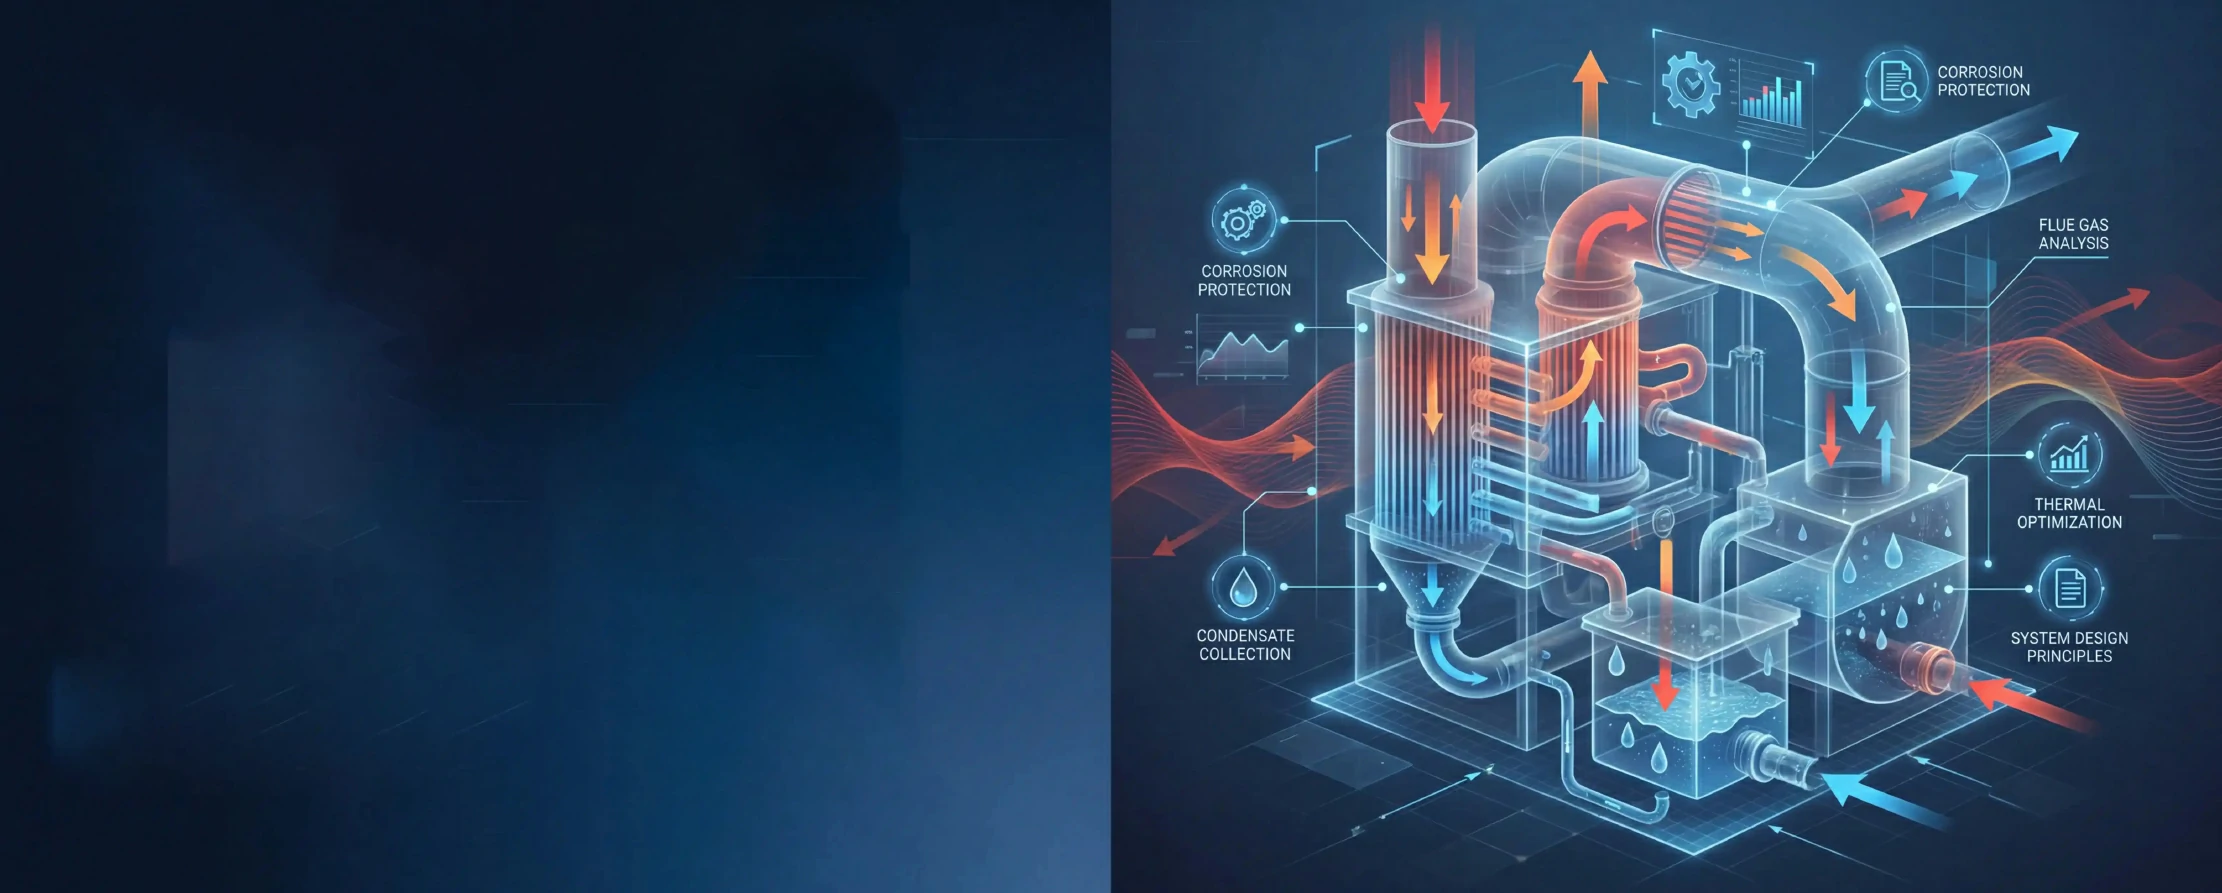
Where condensation occurs, condensate drainage and corrosion protection may also be necessary.
Different technologies are used depending on the waste heat temperature, process requirements, and desired energy output.
Waste heat recovery boilers use hot exhaust gas or process heat to generate steam or hot water.
They are particularly relevant when sufficient thermal energy is available for steam production.
An economizer transfers waste heat from exhaust gas to a water circuit, commonly preheating boiler feedwater.
By increasing feedwater temperature before it enters the boiler, the economizer reduces the additional heat required for steam generation.
Economizers are widely used in industrial boiler systems.
Air preheaters recover exhaust heat and transfer it to incoming combustion air.
Warmer combustion air reduces the fuel energy needed to achieve the required process temperature, subject to the combustion system's operating limits.
Condensing heat exchangers recover heat by cooling exhaust gas to conditions where water vapor condenses.
In addition to sensible heat, they can recover latent heat released during condensation.
These systems may offer additional recovery potential when a sufficiently cool heat sink is available.
However, condensation can introduce corrosion risks, particularly in exhaust streams containing acid-forming components.
Some industrial facilities convert waste heat into electricity through technologies such as steam turbines or Organic Rankine Cycle systems.
These solutions require suitable source temperatures, thermal capacity, and economic conditions.
A waste heat recovery boiler (WHRB) is a boiler that uses thermal energy from an existing industrial exhaust or process stream to generate steam or hot water.
Unlike a conventional fired boiler, which primarily relies on fuel combustion to supply heat, a waste heat recovery boiler utilizes energy already produced by another process.
Some systems operate without additional firing, while others include supplementary firing to meet specific steam requirements.
The operating process typically follows four stages:
Waste heat recovery boilers are commonly associated with gas turbines, industrial furnaces, chemical plants, and other processes producing sufficiently hot exhaust streams.
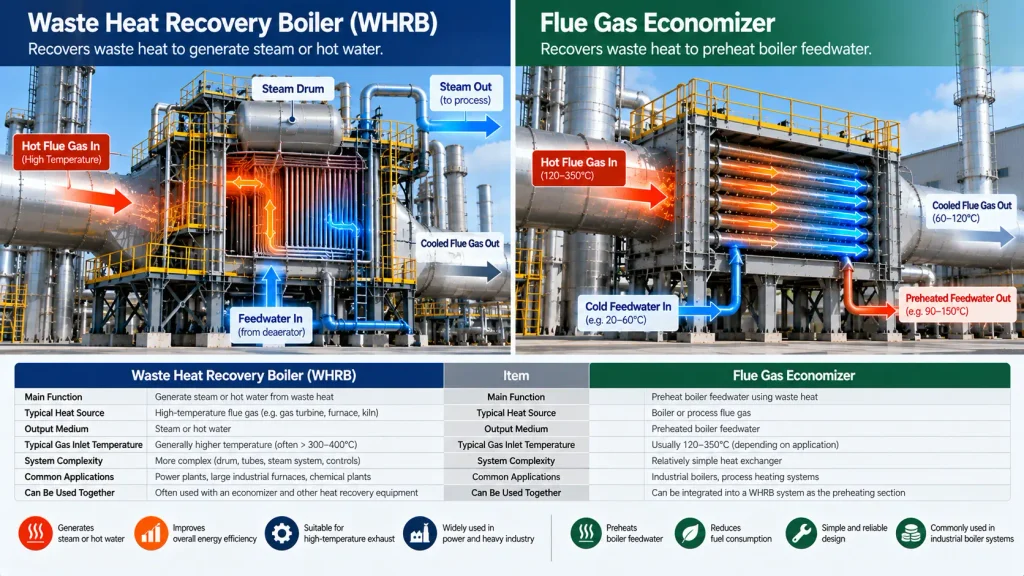
Although both recover waste heat, they perform different functions.
| Feature | Waste Heat Recovery Boiler | Economizer |
| Primary purpose | Generate steam or hot water from waste heat | Preheat water using exhaust heat |
| Typical heat source | Industrial exhaust or process heat | Boiler or process exhaust gas |
| Steam generation | Common in steam-generating designs | Usually not the primary function |
| System complexity | Often includes boiler pressure parts and steam controls | Typically simpler heat exchanger arrangement |
| Main application | Steam generation and process energy recovery | Boiler efficiency improvement |
An economizer may be integrated into a waste heat recovery boiler system, but it is not necessarily a complete waste heat recovery boiler.
This distinction is important when selecting equipment for an industrial project.
Recovered heat can replace part of the energy otherwise supplied by fuel or electricity.
This reduces the additional energy needed for heating, steam generation, or other industrial processes.
Reduced fuel demand can lower energy expenses.
However, total economic performance also depends on equipment costs, maintenance, pumping or fan power, and annual operating hours.
Waste heat recovery increases the useful energy obtained from an existing process.
Instead of allowing residual heat to escape unused, the facility redirects it to productive applications.
When recovered heat displaces additional fuel combustion, associated greenhouse gas emissions can decrease.
The actual reduction depends on the amount of fuel displaced and the characteristics of the industrial system.
Waste heat recovery can connect previously separate industrial processes.
For example, heat discharged from one process may become a useful energy source for another.
This can improve overall plant energy management.
High-temperature exhaust gas generally provides a larger temperature difference for heat transfer.
As the exhaust gas cools, recovering additional heat becomes more difficult.
The temperature difference between the heat source and receiving medium decreases, which may require greater heat transfer area.
At the same time, low-temperature operation can introduce condensation and corrosion risks.
Industrial flue gas may contain sulfur compounds, moisture, chlorides, and other chemically aggressive components.
Under certain conditions, acidic substances can condense on heat transfer surfaces.
These condensates may cause:
The temperature at which corrosive condensation begins depends on the flue gas composition and operating conditions.
For this reason, a heat exchanger designed for clean natural gas exhaust may not be suitable for sulfur-containing or chemically aggressive industrial flue gas.
Dust, ash, and other particles may accumulate on heat transfer surfaces.
These deposits reduce heat transfer performance and increase flow resistance.
A suitable heat recovery system must therefore balance thermal efficiency, corrosion resistance, cleaning accessibility, and allowable pressure drop.
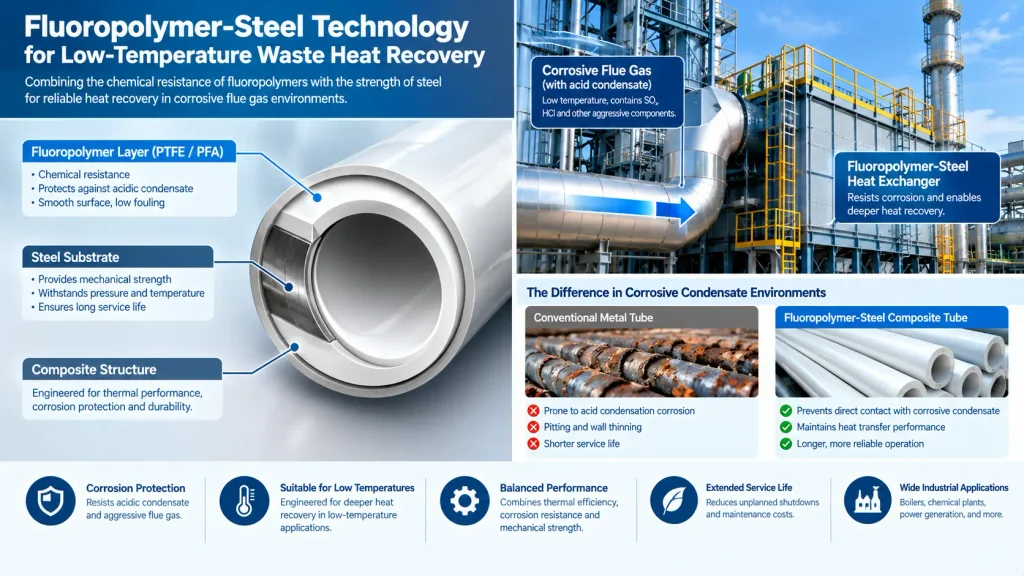
For industrial facilities handling corrosive flue gas, the challenge is not simply recovering heat.
It is recovering heat while maintaining reliable operation under aggressive chemical conditions.
Langteng Thermal focuses on fluoropolymer-steel composite heat exchanger technology for selected industrial flue gas heat recovery applications.
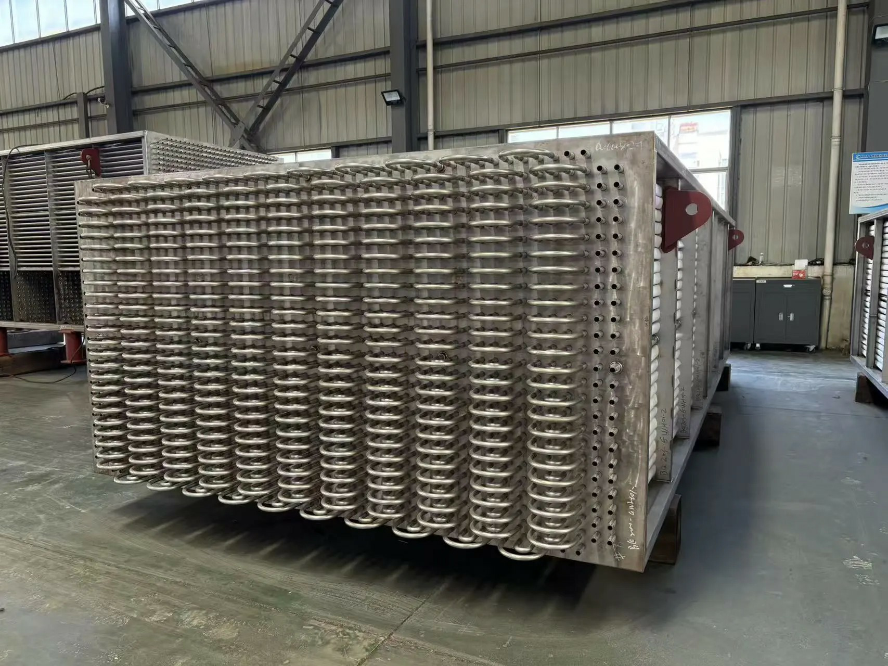
Fluoropolymer-steel composite tubes combine two material functions.
Fluoropolymer protective layer
Fluoropolymers such as PTFE and PFA offer chemical resistance against many industrial substances.
When appropriately engineered, a protective fluoropolymer layer can help reduce direct exposure of the underlying steel to corrosive condensate.
Steel substrate
The steel substrate provides structural support and contributes mechanical strength.
Together, these materials allow the heat transfer surface to be designed for specific corrosive operating environments.
Fluoropolymers have lower thermal conductivity than most conventional heat exchanger metals.
Consequently, a fluoropolymer protective layer adds thermal resistance.
A reliable design must account for this effect through appropriate heat transfer area, material selection, tube configuration, and operating conditions.
The advantage of composite construction is not inherently faster heat transfer.
Its potential value lies in achieving a workable balance between thermal performance, corrosion protection, and long-term reliability.
In suitable applications, corrosion-resistant composite heat exchangers may allow designers to consider lower flue gas outlet temperatures than would be practical with unprotected materials.
This can support additional sensible heat recovery and, where operating conditions permit, condensing heat recovery.
However, the feasibility of deeper cooling must be evaluated together with gas chemistry, heat sink temperature, condensate handling, and downstream equipment compatibility.
Langteng Thermal develops industrial heat transfer equipment for corrosive flue gas and specialized heat recovery requirements.
Designed to recover heat from industrial flue gas and transfer it to water circuits.
Typical applications include boiler efficiency improvement and low-temperature exhaust heat recovery.
Designed for applications where flue gas condensation and corrosive condensate management are important engineering considerations.
These systems can support recovery of additional thermal energy under suitable operating conditions.
Designed to transfer recovered thermal energy to incoming air streams for industrial heating or combustion-related applications.
Equipment configuration and materials must be matched to the actual temperature and gas composition.
Industrial waste heat recovery equipment must be selected according to actual process requirements.
Key engineering parameters include:
| Parameter | Engineering Importance |
| Exhaust Gas Flow Rate | Determines available heat capacity |
| Gas Inlet Temperature | Establishes the thermal starting condition |
| Target Gas Outlet Temperature | Influences heat recovery and condensation risk |
| Gas Composition | Determines corrosion and material requirements |
| Heat Recovery Medium | Defines the intended energy reuse |
| Water or Air Temperature | Influences achievable heat transfer |
| Allowable Pressure Drop | Protects process operation |
| Dust Loading | Influences fouling and cleaning requirements |
| Annual Operating Hours | Affects economic feasibility |
A successful system must consider all these factors rather than focusing only on the maximum theoretical heat recovery.
The most suitable technology depends on the relationship between the available waste heat and the required energy output.
For industrial facilities requiring steam from sufficiently hot exhaust gas, a waste heat recovery boiler may be appropriate.
For boiler feedwater preheating, an economizer may be a more practical solution.
For combustion air heating, an air preheater can provide direct energy integration.
For low-temperature flue gas containing aggressive chemical components, a corrosion-resistant economizer or condenser may be necessary.
The most effective solution is therefore determined by heat source conditions, useful heat demand, material compatibility, and lifecycle economics.
Waste heat recovery works by capturing unused thermal energy from industrial exhaust gas, liquids, or other process streams and transferring it to a useful application through heat exchangers or energy conversion equipment.
Its purpose is to reduce wasted energy, improve overall process efficiency, and lower the additional fuel or electricity required for industrial operations.
A waste heat recovery boiler commonly uses industrial waste heat to generate steam or hot water. An economizer primarily uses exhaust heat to preheat water, often before it enters a boiler.
Yes. Low-temperature waste heat can be used for water preheating, process heating, or other suitable applications. In corrosive flue gas environments, material selection and condensation management are particularly important.
Corrosion-resistant heat exchangers help protect heat transfer surfaces where acidic condensates or chemically aggressive gases could damage conventional materials.
Waste heat recovery is an important strategy for improving industrial energy efficiency.
By capturing thermal energy that would otherwise be discharged, industrial facilities can reduce energy consumption and reuse heat for steam generation, water heating, combustion air preheating, and other processes.
Different technologies serve different purposes.
Waste heat recovery boilers are commonly used for steam generation, while economizers, condensers, and air preheaters provide targeted heat recovery functions.
For low-temperature industrial flue gas, corrosion resistance can become a critical factor in achieving reliable long-term performance.
Fluoropolymer-steel composite technology provides a material approach for selected corrosive heat recovery applications, combining protective fluoropolymer surfaces with steel structural support.
Langteng Thermal provides engineered heat exchanger solutions for industrial flue gas heat recovery.
Contact our engineering team to discuss your exhaust gas conditions, heat recovery objectives, and material requirements.
@ 2025-2026 Langteng Machinery. All Rights Reserved.